

Bucket Elevator Gearbox: Grain Elevator Leg Drive Selection | WGT
A bucket elevator gearbox is sized on one hard rule: the head shaft of a grain leg turns fast - typically 50 to 75 rpm on a belt leg and 20 to 35 rpm on a chain leg - which puts the reduction from a four-pole motor in the two-stage band, not the deep three-stage range a silo auger needs. Everything else that matters is about failure modes: a leg that starts buried, a belt that rolls back when the drive trips, and dust that must never find a hot surface. Choose the frame on those and the speed ratio will almost choose itself.
This guide walks the drive through a working leg: the speed rule and where it comes from, the holdback case that catches a falling belt, the boot start that sizes the frame, and the specification a grain terminal should put in front of a supplier.
What a Bucket Elevator Asks of Its Drive
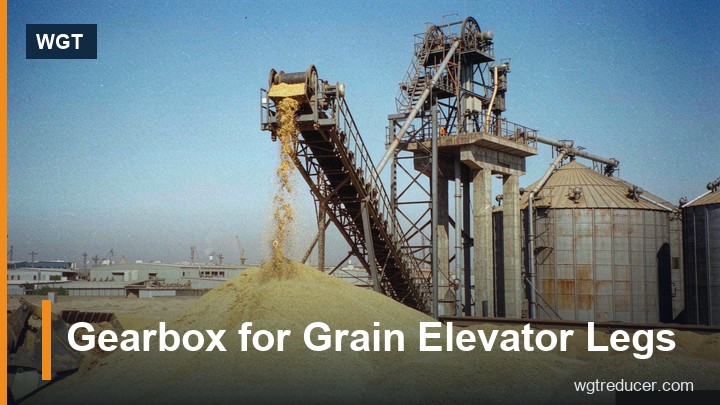
A grain leg is the simplest conveyor in the terminal and the one the site cannot work without: a continuous belt or chain of buckets running up one side of the casing and down the other, lifting grain from the boot to the head. The drive sees a steady, predictable load while the leg runs full.
Steady does not mean gentle. A large leg lifts hundreds of tonnes per hour against thirty or forty metres of height, and the torque at the head shaft is the direct product of that duty. The drive is also permanently exposed - mounted beside the head pulley at the top of the leg, in dust, weather and whatever temperature the building holds.
Three duties set the specification:
- Running torque from the lifting duty, calculable from throughput and lift height to within a few per cent.
- Start-up torque from a leg that stopped with grain in the buckets, which can exceed the running figure several times over.
- Holdback torque - the reverse-load case when the drive trips and the loaded side of the belt tries to run backwards.
The Speed Rule: Why Legs Turn Faster Than You Expect
Bucket speed is chosen for discharge, not for capacity. Grain must leave the bucket at the head pulley by centrifugal throw, and that works only in a narrow band of peripheral speed: too slow and the grain rides over the top and falls back down the up-leg; too fast and it throws too early and lands in the down-leg.
For belt legs the head pulley peripheral speed lands around 2 to 3.5 m/s, which on a 630 mm head pulley is roughly 60 to 105 rpm. Chain legs run slower, because the chain and buckets are heavier and the discharge is gravity rather than centrifugal.
| Leg type | Head shaft speed | Reduction from 1450 rpm | Typical stages |
|---|---|---|---|
| Belt leg, centrifugal discharge | 55–75 rpm | i = 19–26 | Two |
| Belt leg, small pulley | 75–105 rpm | i = 14–19 | Two |
| Chain leg, gravity discharge | 20–35 rpm | i = 41–73 | Two, sometimes three |
| Slow chain leg, large lift | 15–25 rpm | i = 58–97 | Two to three |
The table explains why most bucket elevator gearboxes are two-stage parallel-shaft or right-angle units of moderate ratio - a completely different selection territory from the silo sweep auger at the bottom of the same building, where a level-output right-angle gear unit crawls through a three-stage reduction. One site, two band positions, and the speed rule decides which is which.
Holdback: The Case That Catches a Falling Belt
When a loaded leg trips, the loaded side of the belt outweighs the empty side by tonnes. Without a holdback, that imbalance drives the head shaft backwards, buckets dump into the boot, the boot plugs, and the restart becomes a manual dig-out at the worst hour of the harvest.
Three holdback mechanisms exist, and the choice belongs in the gearbox order, not as an afterthought:
- A centrifugal holdback sprag unit inside the gearbox backstop - the standard answer on modern legs. It engages instantly on reverse rotation and freewheels silently in normal running.
- A ratchet holdback on the head shaft - robust, simpler, but it holds at tooth pitches, so the release into forward running is less smooth.
- A controlled ramp-down by variable frequency drive - workable where the drive electronics are trusted, but it protects nothing when the trip is electrical, which is precisely when the leg is loaded.
The holdback must be rated for the full reverse torque of the loaded leg, which is usually larger than the motor's running torque. This is one of the two figures most often missing from an enquiry - the other being the boot-start condition below.
Boot Starts: The Load That Sizes the Frame
A leg that stops while running full restarts against grain still held in the buckets on the up-leg. The running torque calculation assumes those buckets are empty; they are not. The restart torque can reach three to four times the running figure, and it arrives when the site is already having a bad day.
Sizing honestly on the boot start costs one frame size on a large leg and nothing on a small one. Sizing optimistically costs a sheared key, a tripped protection relay or a stretched belt in the first season - and a key change on a leg head shaft is a half-day job at height.
Two specification habits prevent most of it. First, state on the enquiry whether the leg starts loaded routinely - port terminals and harvest elevators do, inland stores may not. Second, agree the start method: direct-on-line starts hand the full inrush and the full mechanical shock to the train, while a soft start or a crawl-then-run profile with a VFD spreads it. The gearbox frame follows that agreement.
Belt Legs Versus Chain Legs
The transmission choice changes the drive more than any other option in the leg.
Belt legs are lighter, faster and quieter, and they forgive small misalignments. Their head shaft runs in the 55–75 rpm band, so a two-stage unit of modest ratio suits them, and their failure mode under overload is slip rather than shear - the belt protects the train to a degree.
Chain legs carry heavier buckets and run slower, which pushes the ratio deeper and the torques higher per bucket. Their overload behaviour is stiffer: a chain does not slip, so an overload goes through the holdback, the coupling and the gears. A chain leg's gearbox therefore wants the more generous service factor, and the coupling wants a real torque limiter rather than a full-strength solid connection.
Neither choice is wrong, and most terminals run both. What matters for the drive order is that the leg type, the head shaft speed and the overload philosophy are stated together.
Dust: The Discipline Around the Drive
Grain dust is combustible, and a leg head house concentrates it. The gearbox's contribution to the risk picture is small but real: a hot case, a sparking bearing in distress, a failed coupling rubbing its guard.
The controls are ordinary and effective. Keep the case surface temperature unremarkable by choosing the frame with a normal service factor rather than running a small unit hot. Seal the output against dust with a labyrinth or purgeable arrangement, because grain dust is abrasive enough to wear a plain lip seal within a season. House the coupling. And clean the head house on the schedule the insurance surveyor assumes it is kept on, because a dust layer does most of the harm long before any equipment fault.
Housekeeping is also the honest answer to the ATEX question: classification belongs to the plant's engineer, but the gearbox specification that supports it - low surface temperature, sealed bearings, no rubbing points - costs nothing to write into the order and everything to retrofit.
Mounting at the Head of the Leg
Leg head shafts are short and end in outboard bearings, which makes the drive arrangement unusually simple: a right-angle or parallel-shaft unit on a shelf beside the head, keyed to the stub shaft through a spacer coupling.
The shelf deserves a sentence of respect. It carries the drive's weight, the reaction couple and the vibration of a running leg, at a height nobody enjoys visiting. A bracket welded to the leg casing flexes with belt load; a shelf on the building steel does not. The difference shows up as a coupling that stays aligned and a seal that lasts its rated life.
Access matters more than it appears on a drawing. The drive will be serviced from a platform, in weather, with the leg stopped - so lifting lugs on the case, a breather that can be reached without leaning, and a drain plumbed to the shelf edge are worth asking for at order time.
The Numbers a Terminal Should Send
A bucket elevator gearbox enquiry that gets one clean quotation carries:
- Head shaft diameter and keyway, and whether an existing gearbox footprint should be matched.
- Head shaft speed and the leg type - belt or chain - with throughput and lift height.
- Start condition: loaded routinely or not, and the start method agreed with the electrical engineer.
- Holdback requirement, with the reverse torque calculated or at least acknowledged.
- Environment: head house ambient, dust discipline, and whether the unit stands outdoors.
The online selection system takes the speed and torque pair and returns the frame; the holdback rating and the boot-start service factor are the two arguments the returned datasheet will not have for you.
FAQ
Why do grain elevator legs run at 50 to 75 rpm on the head shaft?
Because centrifugal discharge works only in a narrow band of bucket peripheral speed. Below it the grain rides over the pulley and falls back into the up-leg; above it, it throws too early and lands in the down-leg. The speed band sets the ratio, and the ratio places the drive in the two-stage band for most legs.
Does every bucket elevator gearbox need a holdback?
Any leg that lifts a meaningful height loaded needs one, because the imbalance of a loaded side over an empty side will run the head shaft backwards on a trip, dumping grain into the boot. Small legs with short lifts are the exception, and the decision should be made on the reverse torque calculation rather than on habit.
What service factor should I apply for a boot start?
Size the frame on the loaded-restart torque, not on the running figure - on a large leg that is typically one frame above the steady-duty choice. Where the leg starts loaded routinely, the service factor conversation and the start method belong together, because a soft start changes what the train actually sees.
Belt leg or chain leg - which is easier on the gearbox?
A belt leg protects the train by slipping under overload and runs in the easier speed band. A chain leg carries more per bucket and transmits its overloads, so its drive needs the stiffer service factor and a genuine torque-limiting coupling. The choice is usually made by the material and the layout, not by the drive.
A grain leg drive is decided by the speed rule, the holdback and the boot start - in that order - and then it runs for decades on the dust discipline around it. Send the five numbers above and the frame comes back single rather than ranged, which is how an elevator gearbox order should feel from both sides.
